Choosing the right machine involves more than comparing purchase prices. For global buyers, an Aluminum Drawing Machine must match the alloy, inlet size, reduction schedule, and final wire diameter. A bright aluminum rod may enter the line, while smooth and consistent wire should leave it. That result depends on die quality, capstan control, lubrication, cooling, and operator access. Small mismatches can create scratches, ovality, or wire breaks. They also increase material waste.
This guide examines seven machines through practical purchasing criteria. It considers stable output, realistic workloads, maintenance access, and long-term support. Catalog speed alone is not enough. Buyers should request drawing force data, motor details, energy figures, spare-parts information, and commissioning records. Quoted capacity may apply only to one alloy and diameter. It may not. Supplier claims should be compared with factory videos, test samples, inspection reports, and references from similar plants. Some brochures sound precise, yet omit die-life assumptions or actual power consumption.
A reliable shortlist also considers voltage compatibility, operator training, safety systems, documentation, and service coverage. Local support may matter more than a slightly higher rated speed. The cheapest machine is not always economical. One unavailable seal can stop production and delay shipments. These recommendations balance productivity, wire quality, safety, and ownership cost. They are not a substitute for a witnessed trial. That caution matters. Conditions vary. Buyers should verify every technical figure, sample result, and delivery promise before signing a purchase order.
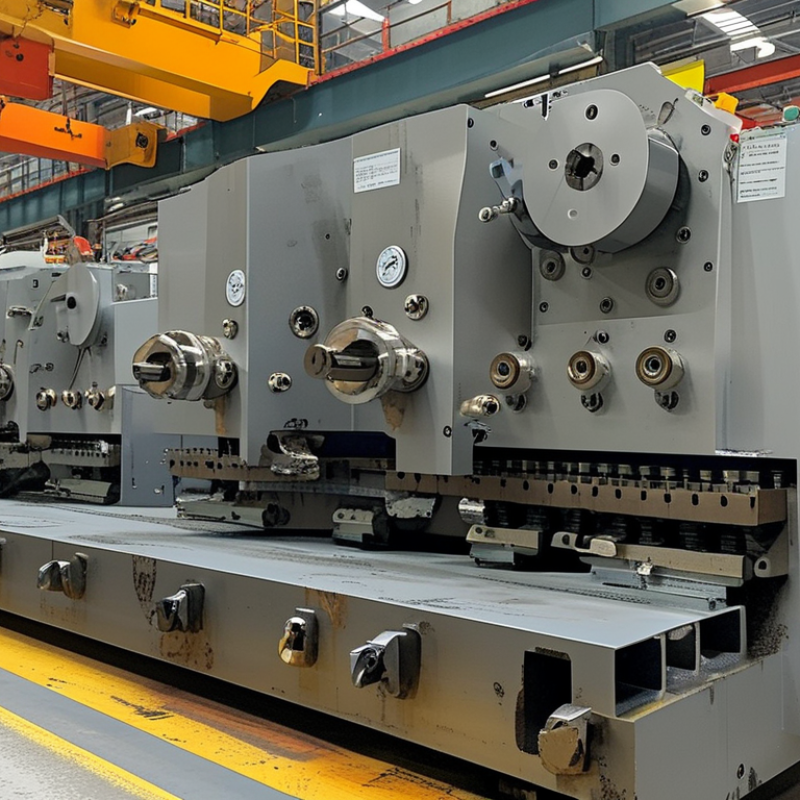
In modern wire manufacturing, aluminum drawing machines reduce rod diameter through controlled dies. They pull aluminum through progressively smaller openings. This improves dimensional accuracy for electrical, construction, and transport applications. A well-adjusted line controls tension, speed, lubrication, and cooling together. Small errors matter. Die misalignment can create scratches, oval sections, or uneven surfaces.
The best machines for global buyers often combine rigid frames, efficient motors, automatic tension control, and accessible maintenance points. Their capstans must handle aluminum’s softness without crushing or marking the wire. Operators monitor elongation, die temperature, current load, and finished diameter during production. Digital records help verify repeatability across shifts. Still, automation cannot replace practical judgment. Sensors can drift, and settings for one alloy may fail on another.
From factory experience, buyers should test each machine with their actual rod size, alloy, target diameter, and production speed. Ask for sample data, safety documentation, spare-part guidance, and operator training details. Energy use deserves attention because continuous drawing can raise operating costs. Maintenance access also affects real output, despite impressive speed claims. I have seen ambitious settings increase scrap instead of capacity. A slower, stable pass may produce better wire and fewer interruptions. Operators should review die wear, surface quality, and tensile results before approving routine production.
What Aluminum Drawing Machines Do in Modern Wire Manufacturing
Aluminum wire drawing machines reduce the diameter of aluminum rod through successive dies while increasing length and improving dimensional consistency. This chart uses a standard 9.5 mm aluminum rod as the starting diameter and shows the cumulative cross-sectional area reduction at seven commonly used drawing targets. Reduction percentages are calculated from the circular wire-area formula: A = πd²/4.
For global buyers, drawing speed should be checked under production load, not brochure maximum. Ask for the stable speed range, acceleration behavior, and output at the target diameter. A line running at 1,200 meters per minute may slow sharply with harder aluminum alloys. That difference affects delivery promises. During a factory trial, watch wire tension, surface marks, and die temperature. Small fluctuations often reveal control problems before rejects become visible.
Capacity needs a practical definition. Check kilograms per hour, coil size, pass arrangement, and changeover time. A machine with high theoretical capacity can lose hours during threading, cleaning, or die replacement. I prefer reviewing a full-shift record rather than one impressive test coil. Include the smallest and largest planned wire sizes. Otherwise, capacity figures remain incomplete. Precision should cover diameter tolerance, ovality, surface finish, and repeatability after restarts. Request measured samples from several coils, not one carefully selected piece.
Energy use deserves equal attention. Compare kilowatt-hours per ton using the same alloy, reduction, speed, and cooling conditions. Measure idle consumption separately. Motors, cooling pumps, and heating systems may draw power during production pauses. Ask whether regenerative braking, efficient drives, or heat recovery are genuinely included. Do not trust one energy number. It may reflect ideal settings. I would leave room for uncertainty because alloy hardness and operator habits change results. That caution is less polished, but more useful for a defensible purchase decision.
Choosing an aluminum drawing machine depends on wire size, alloy, surface quality, and production volume. A single-die machine suits prototypes and frequent size changes. It offers simple control, but output remains limited. Multi-die machines reduce repeated handling and improve throughput. They fit continuous cable production, although setup errors can affect every pass.
Wet drawing machines use lubricant around the dies. They are effective for fine wires and smoother surfaces. Dry drawing machines need less fluid management and work well for medium diameters. A slip-type machine supports high speed with controlled wire tension. A non-slip model delivers stable reduction for larger aluminum conductors. Tubular machines handle specialized profiles, while straight-line machines provide accurate, repeatable drawing for long production runs.
Tips: Check die alignment, cooling capacity, and tension control before comparing speed. Ask for test results using your alloy and target diameter. A machine rated for high speed may perform poorly with soft aluminum. I have seen buyers focus on motor power and overlook lubricant filtration. That mistake can create scratches within hours. Energy data also deserves scrutiny. Published figures may not match factory conditions, especially during frequent coil changes. Leave room for operator training and maintenance access. No machine wins every application.
Choosing among the 7 best aluminum drawing machines requires more than comparing advertised speed. Check the frame, capstan, die holder, and contact surfaces first. Stainless steel and hardened alloys usually resist wear better in demanding production. Ask for material certificates and inspect sample parts. A smooth 9.5 mm aluminum rod should leave the die without scratches, cracks, or uneven diameter. Trial results matter more than polished specifications.
Safety features deserve equal attention. Look for enclosed rotating sections, emergency-stop buttons, door interlocks, overload protection, and clear warning lights. Automation should support workers, not confuse them. A reliable PLC, tension sensor, automatic lubrication, and fault records can reduce setup errors. However, excessive automation may create expensive downtime when technicians cannot access the controls. I have found simple interfaces easier to troubleshoot, though this is not always true for large plants. Verify local electrical compatibility and applicable workplace requirements before ordering.
Tips: Request a live test with your aluminum grade and target diameter. Confirm die-changing time, noise levels, cooling performance, and power consumption. Ask how quickly replacement dies, belts, sensors, and control parts can be supplied. Review the maintenance schedule carefully. Daily cleaning may take only fifteen minutes, but neglected coolant can damage surfaces and affect product quality. A written training plan is useful. Still, operators may need extra practice after installation, especially when settings change between alloys.
Choosing among the seven best aluminum drawing machines requires more than comparing catalog prices. Global buyers should begin with production goals, not machine popularity. Define the incoming rod diameter, target wire size, daily output, and required surface quality. A line making electrical wire needs different controls than one producing precision components.
In plant assessments, I check die count, drawing speed, tension control, lubrication, and annealing stability. These details affect scrap, conductivity, and maintenance time. Ask for measured output data, not only advertised speed. A machine running at 1,200 meters per minute may be unsuitable if frequent stoppages reduce real production. Request sample trials using your aluminum grade and die schedule.
Budget planning should include installation, spare dies, energy use, operator training, shipping, and local service. The purchase price is only one part of ownership. A lower-cost machine can become expensive when replacement parts take weeks to arrive. Buyers should also verify electrical standards, guarding, documentation, and applicable safety requirements in the destination country.
My earlier cost estimates often missed downtime during commissioning. That mistake matters. Leave room for adjustments, testing, and operator learning. A modular machine may justify a higher initial cost when production volumes are expected to grow. However, extra capacity is wasteful when orders remain seasonal. Compare three-year operating costs, warranty conditions, service response times, and realistic payback periods before selecting the final configuration.
Accreditations
ISO 9001 Quality Management
HSE Management Compliant
Products and services comply with relevant Australian (AS) and international (ISO, etc.) Standards.
"*" indicates required fields